

[Cement Raw Material Handling Systems: Understanding Their Function and Design Principles]
For the construction industry, especially in the production of cement, efficient handling of raw materials is crucial. The cement raw material handling system is a critical component in cement plants, responsible for transporting various raw materials such as limestone, clay, and iron ore from storage to the processing units. This system ensures that raw materials are delivered in the right quantity and at the right time, directly impacting the overall efficiency and quality of cement production. In this article, we will explore what these systems are and delve into their design principles, providing a comprehensive understanding for professionals in the field.
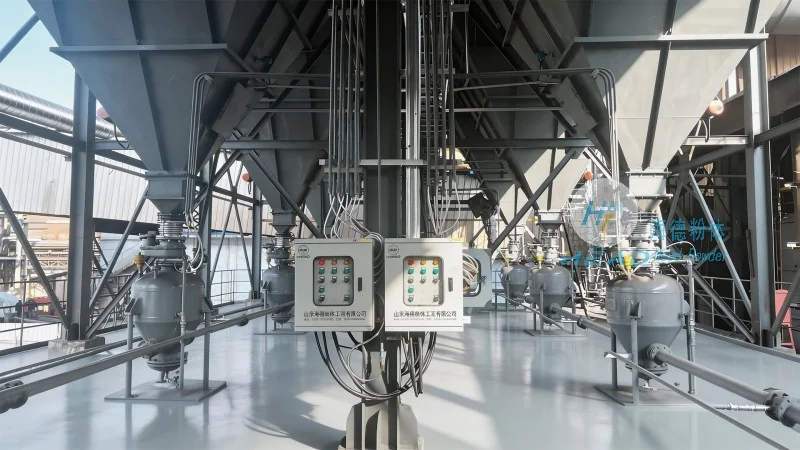
Key Components of Cement Raw Material Handling Systems
The cement raw material handling system typically consists of several key components that work in tandem to ensure smooth material flow. These components include raw material storage facilities, conveyor systems, feeding equipment, and sometimes crushing or grinding units. Each component plays a vital role in the entire process. For instance, storage silos or stockpiles are used to store raw materials, ensuring a steady supply. Conveyor belts or bucket elevators then transport the materials from storage to the processing area. Feeding devices, such as rotary feeders or belt feeders, control the flow rate of materials into the next stage of processing. In some cases, pre-crushing or grinding equipment may be integrated to reduce the size of raw materials before they enter the kiln system.
Design Principles for Efficient Material Handling
The design of a cement raw material handling system is based on several key principles aimed at maximizing efficiency, minimizing energy consumption, and ensuring safety. One of the primary principles is the optimization of material flow, which involves designing a layout that minimizes the distance materials need to travel and reduces the number of transfer points. This reduces energy consumption and the risk of material loss or degradation. Another important principle is the selection of appropriate equipment based on the characteristics of the raw materials. For example, heavy and abrasive materials like limestone may require stronger conveyor belts and more robust feeding equipment to prevent wear and tear. The system design also considers the need for proper dust control and environmental protection, as cement raw materials can generate significant dust during handling. This is achieved through the use of dust collection systems and enclosed conveyor systems.

Role of Material Handling in Cement Production
The cement raw material handling system is integral to the entire cement production process. Raw materials are the foundation of cement, and their quality and consistency directly affect the final product. The handling system ensures that raw materials are processed in a controlled manner, maintaining the required chemical composition and particle size. This consistency is vital for achieving the desired cement properties, such as strength and durability. Additionally, the system contributes to the overall productivity of the cement plant by enabling continuous and uninterrupted material flow. By reducing downtime and minimizing material losses, the handling system helps in maintaining a stable production schedule and meeting market demands efficiently.

HeadPowder's Expertise in Cement Raw Material Handling
Shandong HeadPowder Engineering Co., Ltd. (HeadPowder) is a leading provider of engineering solutions for cement raw material handling systems. With years of experience in the industry, HeadPowder specializes in designing and manufacturing customized systems tailored to the specific needs of cement plants. The company's team of experts works closely with clients to understand their production requirements and develop solutions that enhance efficiency and reduce operational costs. HeadPowder's systems are designed based on the latest technology and industry standards, ensuring reliability and durability. The company's commitment to quality and customer satisfaction has made it a trusted partner for many cement manufacturers in China and beyond. HeadPowder's expertise covers the entire range of raw material handling, from storage and conveyance to feeding and processing, providing comprehensive solutions for cement production facilities.
Conclusion
In conclusion, the cement raw material handling system is a critical component in cement production, responsible for the efficient and safe transport of raw materials. The design principles behind these systems focus on optimizing material flow, selecting appropriate equipment, and ensuring environmental compliance. The role of such systems extends beyond mere transportation, as they directly impact the quality and productivity of cement production. Companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in providing advanced and reliable handling solutions that meet the evolving needs of the cement industry. By investing in efficient raw material handling systems, cement manufacturers can enhance their operational performance and maintain a competitive edge in the market.