

Working Principle and Features of Small Stone Powder Conveyors
Small stone powder conveyors are essential equipment in various industrial applications, designed to efficiently transport fine powders and granular materials. These systems are engineered to handle materials like small stones, powders, and other particulate substances with precision and reliability. The technology behind these conveyors combines mechanical design with advanced control systems to ensure smooth and continuous material movement, making them indispensable in sectors such as mining, construction, and chemical processing.

Working Principle of Small Stone Powder Conveyors
The operation of small stone powder conveyors is based on a combination of mechanical and pneumatic principles. Typically, these systems utilize a hopper to collect the material, which is then fed into a conveyor tube or a series of rotating components. The core mechanism often involves a screw or auger that rotates to push the material forward, or a pneumatic system that uses compressed air to create a flow of material through a duct. The design allows for both horizontal and vertical transport, adapting to different spatial constraints in industrial settings. The conveyor's speed and direction can be controlled via an electric motor or a pneumatic actuator, providing flexibility in material handling. This dual approach ensures that the system can handle a wide range of particle sizes and material densities, from fine powders to small stone fragments.
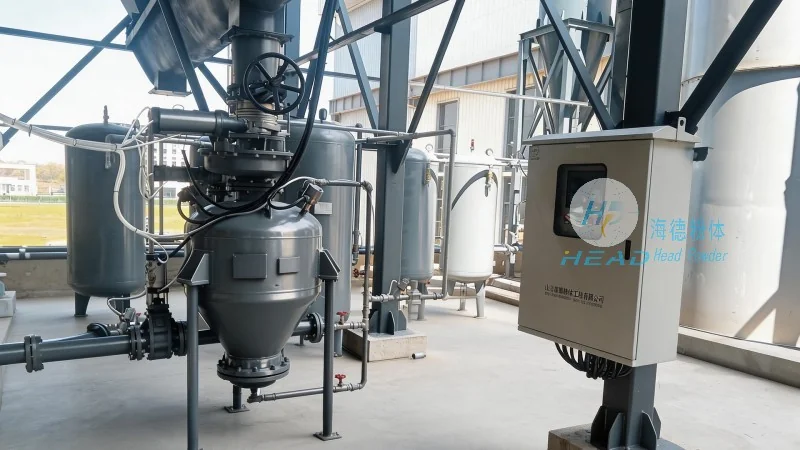
Key Features of Small Stone Powder Conveyors
Small stone powder conveyors are characterized by several key features that enhance their performance and usability. Firstly, their compact design makes them suitable for installation in confined spaces, which is a significant advantage in modern industrial facilities where space optimization is critical. The equipment is also built with durable materials, such as stainless steel or high-grade plastic, to withstand the abrasive nature of small stones and powders, reducing wear and tear over time. Another notable feature is the adjustable speed control, which allows operators to modify the conveyor's output based on production needs, ensuring efficient material flow without overloading the system. Additionally, these conveyors often include safety features like overload protection and emergency stop buttons, enhancing operational safety and compliance with industrial standards. The modular design of many models enables easy maintenance and replacement of components, reducing downtime and maintenance costs. Furthermore, the systems are equipped with monitoring systems that provide real-time data on material flow and system performance, allowing for proactive maintenance and optimization.

Applications and Benefits in Industrial Settings
Small stone powder conveyors find extensive applications across various industries, contributing to improved productivity and operational efficiency. In the mining industry, they are used to transport crushed stone and fine powders from processing plants to storage or shipping areas. The construction sector benefits from these conveyors for transporting cement, sand, and other building materials to job sites, ensuring consistent supply and reducing manual labor. In chemical processing, the equipment is crucial for handling powders like calcium carbonate or other fine chemicals, maintaining product quality and preventing contamination. The primary benefits of using small stone powder conveyors include increased throughput, reduced labor costs, and improved safety compared to traditional manual handling methods. The systems also minimize material loss and contamination, which is vital in industries where product purity is a priority. Furthermore, the energy efficiency of modern conveyor designs helps lower operational costs, making them a cost-effective solution for long-term material handling needs.

Conclusion and Company Information
Small stone powder conveyors represent a sophisticated solution for efficient material transport in industrial environments. By integrating advanced mechanical and pneumatic technologies, these systems offer reliable performance, adaptability, and durability. The key features, such as compact design, adjustable speed, and safety mechanisms, make them suitable for diverse applications while ensuring operational efficiency and safety. As industrial demands for efficient material handling continue to grow, the role of small stone powder conveyors becomes increasingly vital. Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializes in the design, production, and supply of high-quality small stone powder conveyors. With a commitment to innovation and customer satisfaction, the company provides tailored solutions that meet the specific needs of various industries. HeadPowder's products are engineered to deliver optimal performance, ensuring that clients can achieve their production goals with minimal downtime and maximum efficiency. The company's location in Shandong, China, allows for easy access to raw materials and a skilled workforce, supporting the consistent delivery of reliable and durable conveyor systems. Whether for mining, construction, or chemical processing, HeadPowder's small stone powder conveyors offer a dependable solution for material handling challenges.